If you’ve ever worked with industrial components—whether you’re a maintenance supervisor, a machine shop owner, or a procurement manager—you know that keyways are the unsung heroes of power transmission. They’re those small, precision-cut grooves on shafts and hubs that keep gears, pulleys, and sprockets from slipping off, transferring torque smoothly in everything from conveyor systems to wind turbine gearboxes. For us, as a keyway milling supplier, our core promise is not just cutting keyways to spec—it’s delivering parts that don’t fail. And that starts long before we fire up our CNC mills: it starts with a rigorous, step-by-step risk assessment. Keyway Milling
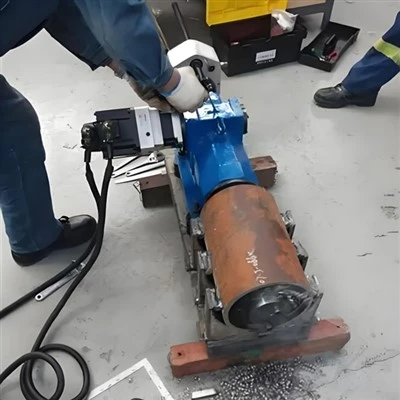
A lot of people think risk assessment is just a box-ticking exercise to satisfy OSHA or ISO standards. But for our team, it’s how we protect our clients, our workers, and our own reputation. Last year, a small manufacturing client came to us with a rush order for 200 keyways on steel shafts for a packaging line. They’d used a different supplier who’d cut the keyways 0.012 inches too shallow. When the line ran, the pulley slipped, the packaging came off, and they lost $12,000 in a single shift. That’s why we don’t cut corners on risk assessment. It’s not just about avoiding mistakes—it’s about building trust with the people who rely on our work every day.
Let me walk you through how we do it, the way we’ve refined it over 18 years in the business.
First, we start with pre-material risk validation. Keyway milling doesn’t exist in a vacuum—it depends entirely on the material we’re working with, its condition, and what the keyway will be used for. I’ve seen so many issues start here because a client says, “Just use standard steel, right?” But standard steel for a garden hose reel is way different from high-tensile alloy for a crane hoist, and those differences change everything.
Our first step in pre-material risk assessment is to confirm three key things: material hardness, shaft dimensional integrity, and the application’s load requirements. Hardness is huge. If a shaft is too soft, the keyway will deform under torque—over time, that groove will stretch, and the part will fail. If it’s too hard, our cutting tools will chip, leading to rough, inconsistent keyways. We use a portable hardness tester to verify every incoming batch, not just a random sample. Last quarter, we got a shipment of 4140 steel that tested 15 HRC softer than the spec. If we’d milled keyways on those shafts, they would have failed in less than six months under the 2,000 ft-lb load the client needed. We sent the material back, no questions asked—even though it delayed their order by two days. It was the right call.
Next, we check the shaft’s dimensional accuracy. A shaft with a bent diameter or out-of-round surface will throw off the milling machine’s alignment, leading to keyways that are off-center or improperly dimensioned. We use a coordinate measuring machine (CMM) for critical parts, but for smaller runs, a dial indicator works. We also confirm the keyway’s purpose: is it a static keyway (for gears that don’t move) or a sliding keyway (for pulleys that need to shift)? Sliding keyways need extra width tolerance to prevent binding, and we factor that into our risk assessment early. If we’d missed that a client needed a sliding keyway and cut it to static specs, their pulley would have seized up, costing them downtime and repair costs. That’s a risk we eliminate before we even set up the machine.
Once the material is cleared, we move to process risk assessment. This is where we map out every step of the milling operation to catch potential failures before they happen. Our milling process has five core steps: fixture setup, tool selection, feed and speed calibration, roughing, and finishing. Each step has its own risks, and we flag them one by one.
Fixture setup is where alignment happens. If the shaft isn’t held securely in the vice or collet, it will move during milling, leading to a keyway that’s too deep on one side or crooked. We use hydraulic vises for most parts, but for high-volume runs, we test collet concentricity every 50 shafts. Last year, a new operator forgot to tighten the collet on a batch of 50 shafts. We caught the issue during a pre-process check, thanks to a simple test run on a scrap shaft. If we’d milled all 50, we would have had to scrap the entire batch at a cost of $3,000 and miss the client’s deadline. That’s why we built in a rule: every setup gets a test cut, and the dimensions are verified before we run production.
Tool selection is another big one. Keyway milling uses end mills, and choosing the wrong tool can lead to broken tools, rough surfaces, or dimensional errors. We match the tool’s diameter and material to the shaft and the keyway depth. For example, for a 1-inch deep keyway on a 4-inch diameter shaft, we use a carbide end mill with a 0.75-inch diameter—too small, and the end mill will flex, leading to a tapered keyway; too big, and we’ll have to make multiple passes that increase the risk of tool breakage. We also consider the number of flutes. For soft aluminum, we use 4-flute end mills for a smoother finish; for hard steel, we use 3-flute end mills to reduce tool load. A few months ago, we tried using a 4-flute end mill for a batch of tool steel shafts. The tool ran too hot, chipped halfway through the first pass, and left a burr that required secondary finishing. We switched to a 3-flute tool, and the error rate dropped to zero. That’s the kind of small, targeted change that comes from thorough risk assessment.
Feed and speed calibration is where a lot of novice shops go wrong. Too fast, and the tool breaks; too slow, and the material work-hardens, making it harder to finish the keyway and increasing wear on the machine. We use the material’s hardness and the tool’s manufacturer guidelines to set our feeds and speeds, but we also add a 10% safety buffer for high-torque applications. For a 30 HRC steel shaft, for example, the recommended speed is 1,500 RPM and a feed rate of 0.015 inches per tooth. We drop the speed to 1,350 RPM and lower the feed rate to 0.012 inches per tooth to reduce the risk of tool deflection. It adds a little time to the process, but it eliminates the risk of errors that would require reworking or scrapping parts.
Roughing and finishing passes are the final steps in process risk. Roughing removes most of the material quickly, but too aggressive a pass can cause the shaft to vibrate, leading to dimensional inaccuracy. Finishing needs to hit the exact spec—usually ±0.001 inches for most applications. We always leave 0.005 inches for the finishing pass, even if the roughing pass looks right. That extra buffer lets the tool cut cleanly without being affected by any minor imperfections from the rough pass. Once the finishing pass is done, we measure the keyway’s width, depth, and position using a micrometer and a height gauge. If it’s even 0.0005 inches off, we flag it as a risk—unless we can adjust it, we scrap it. We’d rather scrap one part than deliver 199 bad ones, because the damage to our reputation would be way worse.
Then there’s the human factor risk, which is the one most shops overlook. At the end of the day, keyway milling is done by people—our operators, our quality control team, even our sales engineers who talk to clients. Human error is the top cause of keyway failures, according to a 2022 study by the Precision Machining Association. That’s why we invest in training and checkpoints that reduce risk at every stage.
For our operators, we do monthly refreshers on risk assessment protocols, not just on machine operation. We’ve built a simple checklist for every operator to use before they start a job: Did we verify the material hardness? Did we run a test cut? Did we confirm the keyway spec with the client? If any of those answers are no, they can’t start the machine. We also rotate operators between high-risk jobs (like milling keyways on wind turbine shafts) and lower-risk jobs, to prevent burnout and keep focus high. Burnout is a big one—when an operator is tired, they’re more likely to skip a step. We limit shift overtime to 10 hours a week, and we schedule regular breaks to keep everyone sharp.
Our quality control team is a separate group from the operators, so there’s no bias when checking parts. Every batch of 20 or fewer parts gets 100% inspection; for batches over 20, we inspect 10% plus the first and last parts. We also do random audits on finished parts, even after they leave our shop. Last year, we audited a batch of 100 keyways for a conveyor system and found a keyway that was 0.002 inches too wide. We called the client, picked up the parts, re-milled the bad one, and delivered the whole batch two days early. They ended up giving us a 20% larger order because they trusted us to catch mistakes they would have missed.
We also include our clients in the risk assessment process. We ask for more information than just “need a keyway cut on a 2-inch shaft.” We ask: What’s the operating load? How many hours a day does the component run? Is it in a corrosive environment? All of these factors change the risk profile of the part. A keyway for a conveyor that runs 24/7 in a food processing plant needs a tighter tolerance than a keyway for a machine that runs 8 hours a day in an office. A few months ago, a client asked for a keyway on a shaft that would be installed in a saltwater desalination plant. We added a 0.003-inch width tolerance to prevent corrosion buildup, and used a coated end mill to resist saltwater damage. If we’d used a standard spec, the keyway would have corroded in 18 months, leading to a shutdown that would have cost the client millions. That’s the value of bringing the client into the risk assessment, not just taking their order.
Now, I know some of you might be thinking: This sounds like a lot of work. Why not just cut the keyways and fix any mistakes later? Let me put that in perspective. A bad keyway costs us time, money, and reputation. If a part fails in the field, we’re responsible for replacing it, and we might lose the client forever. Last year, a shop in Ohio tried to skip risk assessment, and a keyway failure shut down a local manufacturer’s packaging line for 3 days. The manufacturer sued, and the shop went out of business. That’s the risk of cutting corners. For us, a $10,000 order that takes an extra hour for risk assessment is way better than a $50,000 lawsuit and a ruined reputation.
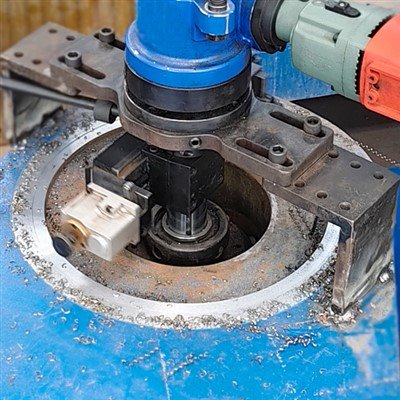
At the end of the day, our job as a keyway milling supplier isn’t just to cut grooves in metal. It’s to make sure those grooves hold when the machine is running, when the load is high, when the environment is tough. Risk assessment is how we turn a basic machining job into something reliable. If you’re in need of keyway milling services, whether for a custom one-off part or a high-volume production run, we’re here to work with you to assess your specific risks and deliver parts that stand the test of time. Reach out to our team to discuss your project and get a quote tailored to your needs.
Line Boring Accessories References
- Precision Machining Association. (2022). Keyway Defect Root Cause Analysis and Risk Mitigation.
- American Society of Mechanical Engineers (ASME). (2019). B106.1M-2019: Key Joints for Transmission Shafts.
- Occupational Safety and Health Administration (OSHA). (2021). Machine Guarding Guidelines for Milling Operations.
- Tooling & Manufacturing Association (TMA). (2023). Carbide End Mill Selection for Keyway Milling Applications.
- International Organization for Standardization (ISO). (2020). ISO 14691:2020 – Mechanical Vibration – Evaluation of Machine Tools.
Shangqiu JDA Machinery Technology Co., Ltd.
With abundant experience, we are one of the most professional keyway milling manufacturers and suppliers in China. We warmly welcome you to buy cheap keyway milling for sale here from our factory. Quality products and reasonable price are available.
Address: No. 55 Pingyuan Middle Road, Liangyuan District, Shangqiu, Henan, China
E-mail: sales@jdamachines.com
WebSite: https://www.jdamachines.com/
